Aluminium polishing and satin finishing
Aluminium polishing and satin finishing in Mataró, near Barcelona
Speak to a technician. Monday to Friday, 8:00 to 17:00 (CET).
The process
What you see is decided before anodising
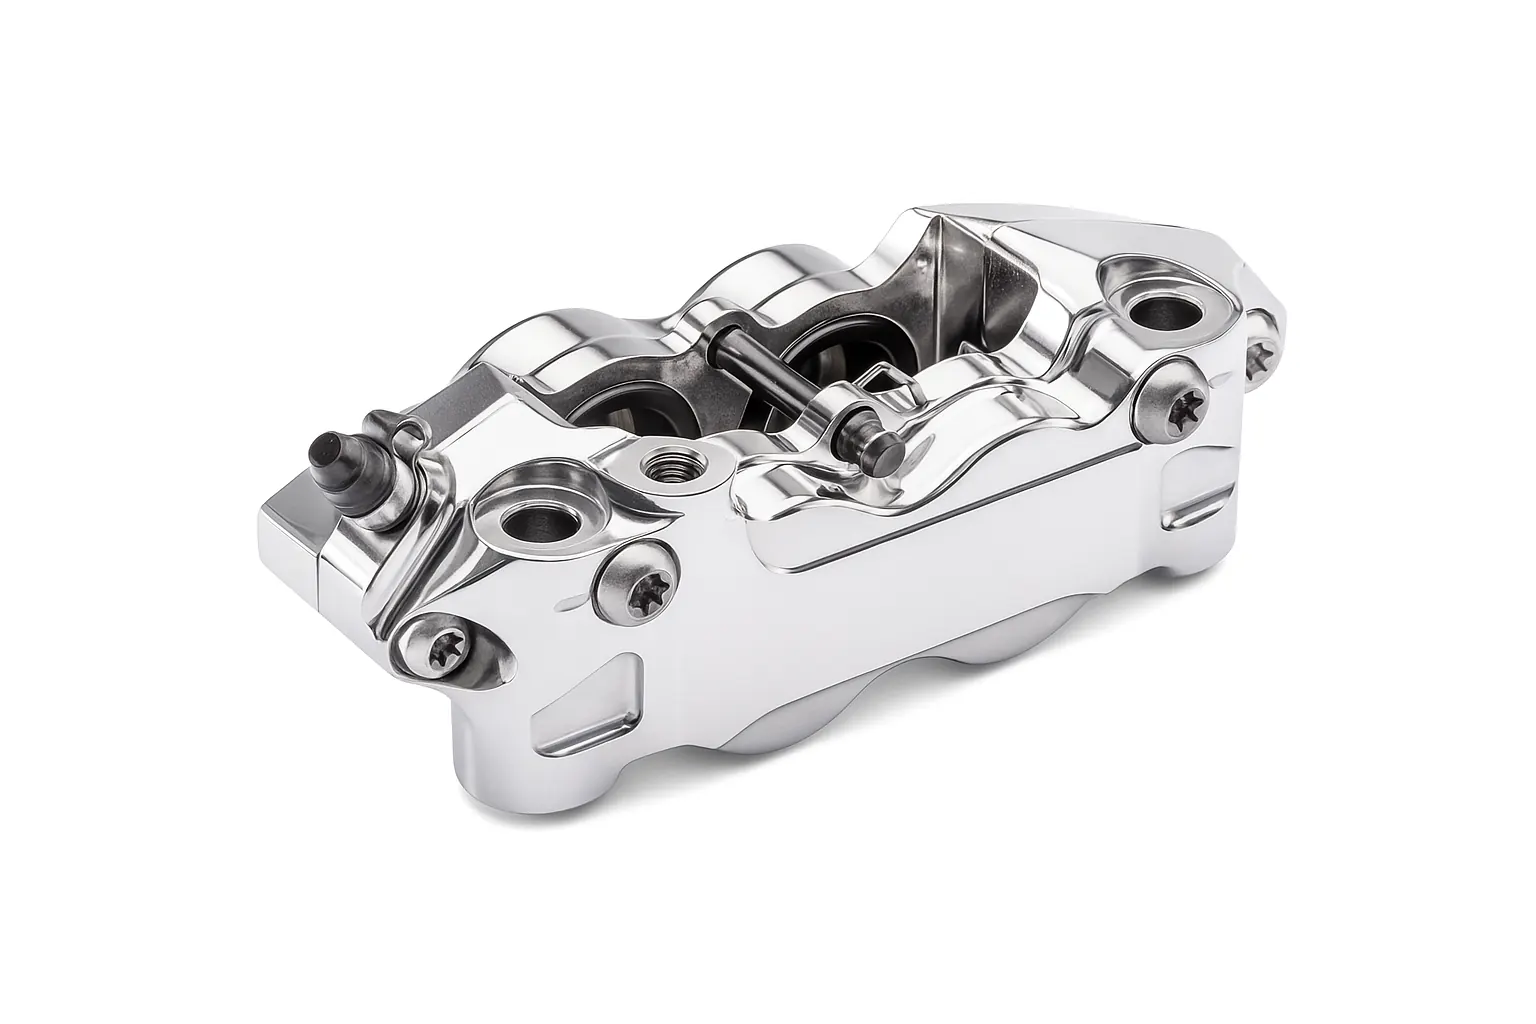
Every part looks the same: the same gloss and the same grain, running the same way. We remove machining marks and leave the part satin, brushed, matt or mirror finished, ready for anodising.
Anodising hides nothing: a machining scratch or an uneven satin finish shows through the layer. The gloss and texture of the finished part are decided at the polishing stage.
We agree with you the gloss, the roughness and the grain direction of every visible face. We validate it on a test part, and the run repeats exactly the same.
- The same gloss and grain across the whole run
- Removes marks and scratches before anodising
- Satin, brushed, mirror or matt
- Roughness and gloss measured against your drawing
Methods
Finishes
Depending on the look you want and what comes next.
Satin and brushed
Fine lines that hide marks and fingerprints. The most common finish before anodising.
- Grain and direction set on the drawing
- The same look from order to order
Suitable for: Visible parts · Before anodising or painting
Bright or mirror polishing
Maximum gloss, with a sequence of wheels and compounds.
- Shows fingerprints and scratches more
- Protection against micro-scratches
- Heat control on thin parts
Suitable for: High-end parts · High reflectivity
Micro-finishing and vibratory finishing
Many parts at once with ceramic or plastic media: softens edges, removes micro-burrs and leaves an even matt finish.
- To be validated on parts with closed cavities
- Cycle time and media mix fixed
Suitable for: Small and medium runs · Micro-deburring · Even matt finish
Preparation for treatment
Roughness and cleanliness set so that anodising or paint grips and comes out the same on every part.
- No compound or abrasive residue
- Cleaning and handling guidelines
Suitable for: Anodising · Liquid paint or powder coating
Quality control
What we control
What it takes for the last part to match the first.
Roughness (Ra/Rz)
To drawing, measured before and after at fixed points.
More stable on an even prior finish.
Reference standards: ISO 4287 · ISO 4288
Typical values
- Target Ra: To drawing
- Measurement direction: Parallel or perpendicular to the grain
How we check it
- Points and direction fixed
- Measurement before and after
- Delivered with the measurements
Gloss and uniformity
No haze or orange peel, inspected in a light booth.
Reference standards: ISO 2813
Typical values
- Gloss: GU at 60° · ISO 2813
- Target: Per part
How we check it
- Visual inspection checklist
- Protection against scratches
Grain direction
The same orientation on every visible face and clean transitions at the edges.
Typical values
- Grit: P120–P600 (as a guide)
- Pattern: Linear or mixed
How we check it
- Orientation templates
- No swirl marks
- Photos with the direction marked
Cleanliness
No compound residue or abrasive dust to spoil the anodising or paint.
Typical values
- Protection: Gloves and film
How we check it
- Final rinse and clean
- Lint-free packaging
Edges and dimensions
We control edge rounding, make sure thin sheet does not distort with heat, and protect threads and fits.
Particular care with threads and H7/H8 fits.
Typical values
- Critical areas: Masked
How we check it
- Pressure and time fixed
- Measurements in the areas you mark
Comparison
Polishing, electropolishing or anodising?
Each one solves a different problem.
Maximum gloss on a visible face
Mirror polishing.
- Edge rounding must be validated
- Shows fingerprints
Even brightness across the whole part
Electropolishing: it reaches cavities too.
- Removes a few microns
- Even brightness
Colour and protection
Anodising, over good polishing or satin finishing.
- Needs an even prior finish
- Colour repeatable between orders
How we work
From sample to production run
Lead times are for guidance: they depend on volume, workload and any tests the project requires.
Call and quotation
Under 24 h
You tell us which faces are visible, the finish you want (ideally with a sample) and whether it will be anodised or painted afterwards.
Test part
About 72 h
We finish a part so you can approve gloss, texture and grain direction before the run.
Production run
5–10 working days
The same route you approved on the sample, with a control plan per part family and records for every batch.
Delivery
At our plant or by carrier
Final inspection, a certificate of conformity if you ask for it, and packaging that protects the finish.
Frequently asked questions
Frequently asked questions
Satin or mirror?
Satin leaves fine lines and a moderate gloss, and hides fingerprints and small marks. Mirror gives maximum gloss but shows everything. For parts that are handled a lot, we usually recommend satin.
Do machining marks show after anodising?
Yes, anodising does not hide them. That is why it is worth polishing or satin finishing first. If you show us the part, we will tell you which prior finish it needs.
How are roughness and gloss set?
We agree the target Ra and gloss with you, measure before and after and validate it on a test part in a light booth. The run repeats that same route.
Can I anodise or paint afterwards?
Yes, and the prior finish decides the result. We take care over cleanliness and grain direction so that the layer or the paint grips and looks the same.
Does it affect tolerances?
It can round edges or remove a few microns. We protect critical areas and measure the ones you mark.
Do you supply a certificate?
Yes. A certificate of conformity for every batch, with the process records, photos and roughness and gloss measurements we agree.
How long does it take?
Samples or the pilot run in about 72 hours (48–72 h). Production runs in 5 to 10 working days, as a guide, depending on volume and workload. More than 99% of our deliveries leave on time.
Sectors
Where we apply it
Industrial design
Products, lighting and furniture with colour, gloss and texture approved on a sample and repeated in every order.
Find out more
Automotive
Visible and technical parts for automotive and e-mobility suppliers, with the same colour and the same paperwork in every batch.
Find out more
Engineering and machinery
Machined parts, tooling and brackets anodised without going out of tolerance, with lead times that do not slow your delivery.
Find out more
Which finish are you after?
We tell you what preparation your part needs to look the way you want after anodising. Call +34 937 55 62 77 and speak to a technician: they will advise you and give you a price. Monday to Friday, 8:00 to 17:00 (CET). If you prefer, leave us your number and we will call you back within the hour.
Speak to a technician. Monday to Friday, 8:00 to 17:00 (CET). Leave your number and we will call you back within the hour.
Direct contact
- Phone
- +34 937 55 62 77
- bucisl@bucisl.com
- Plant
- Carrer dels Remences, 114, 08304 Mataró (Barcelona)